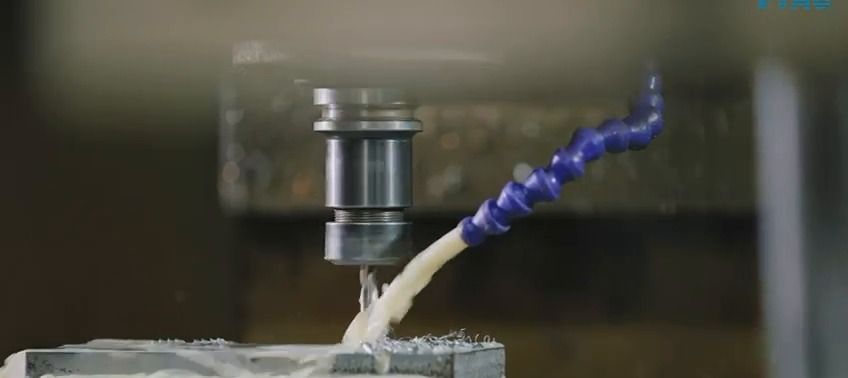
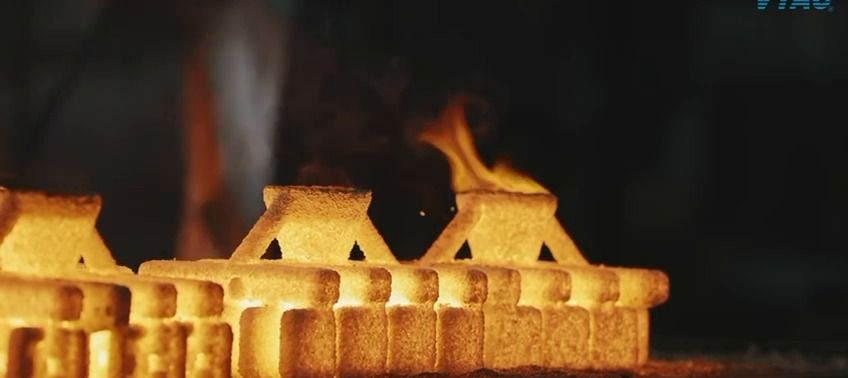
Casting, Forging & Tooling
In-House Tooling, Casting and Forging.
Our tooling team works beside casting and hot forging, so a drawing or sample becomes a repeatable component with fewer handovers.
Read the story: Casting, Forging & ToolingManufacturing
At our factory in Thai Binh, Vietnam, tooling, casting, forging, CNC machining, polishing, plating, assembly and inspection work as one system for repeatable glass fittings and OEM hardware.
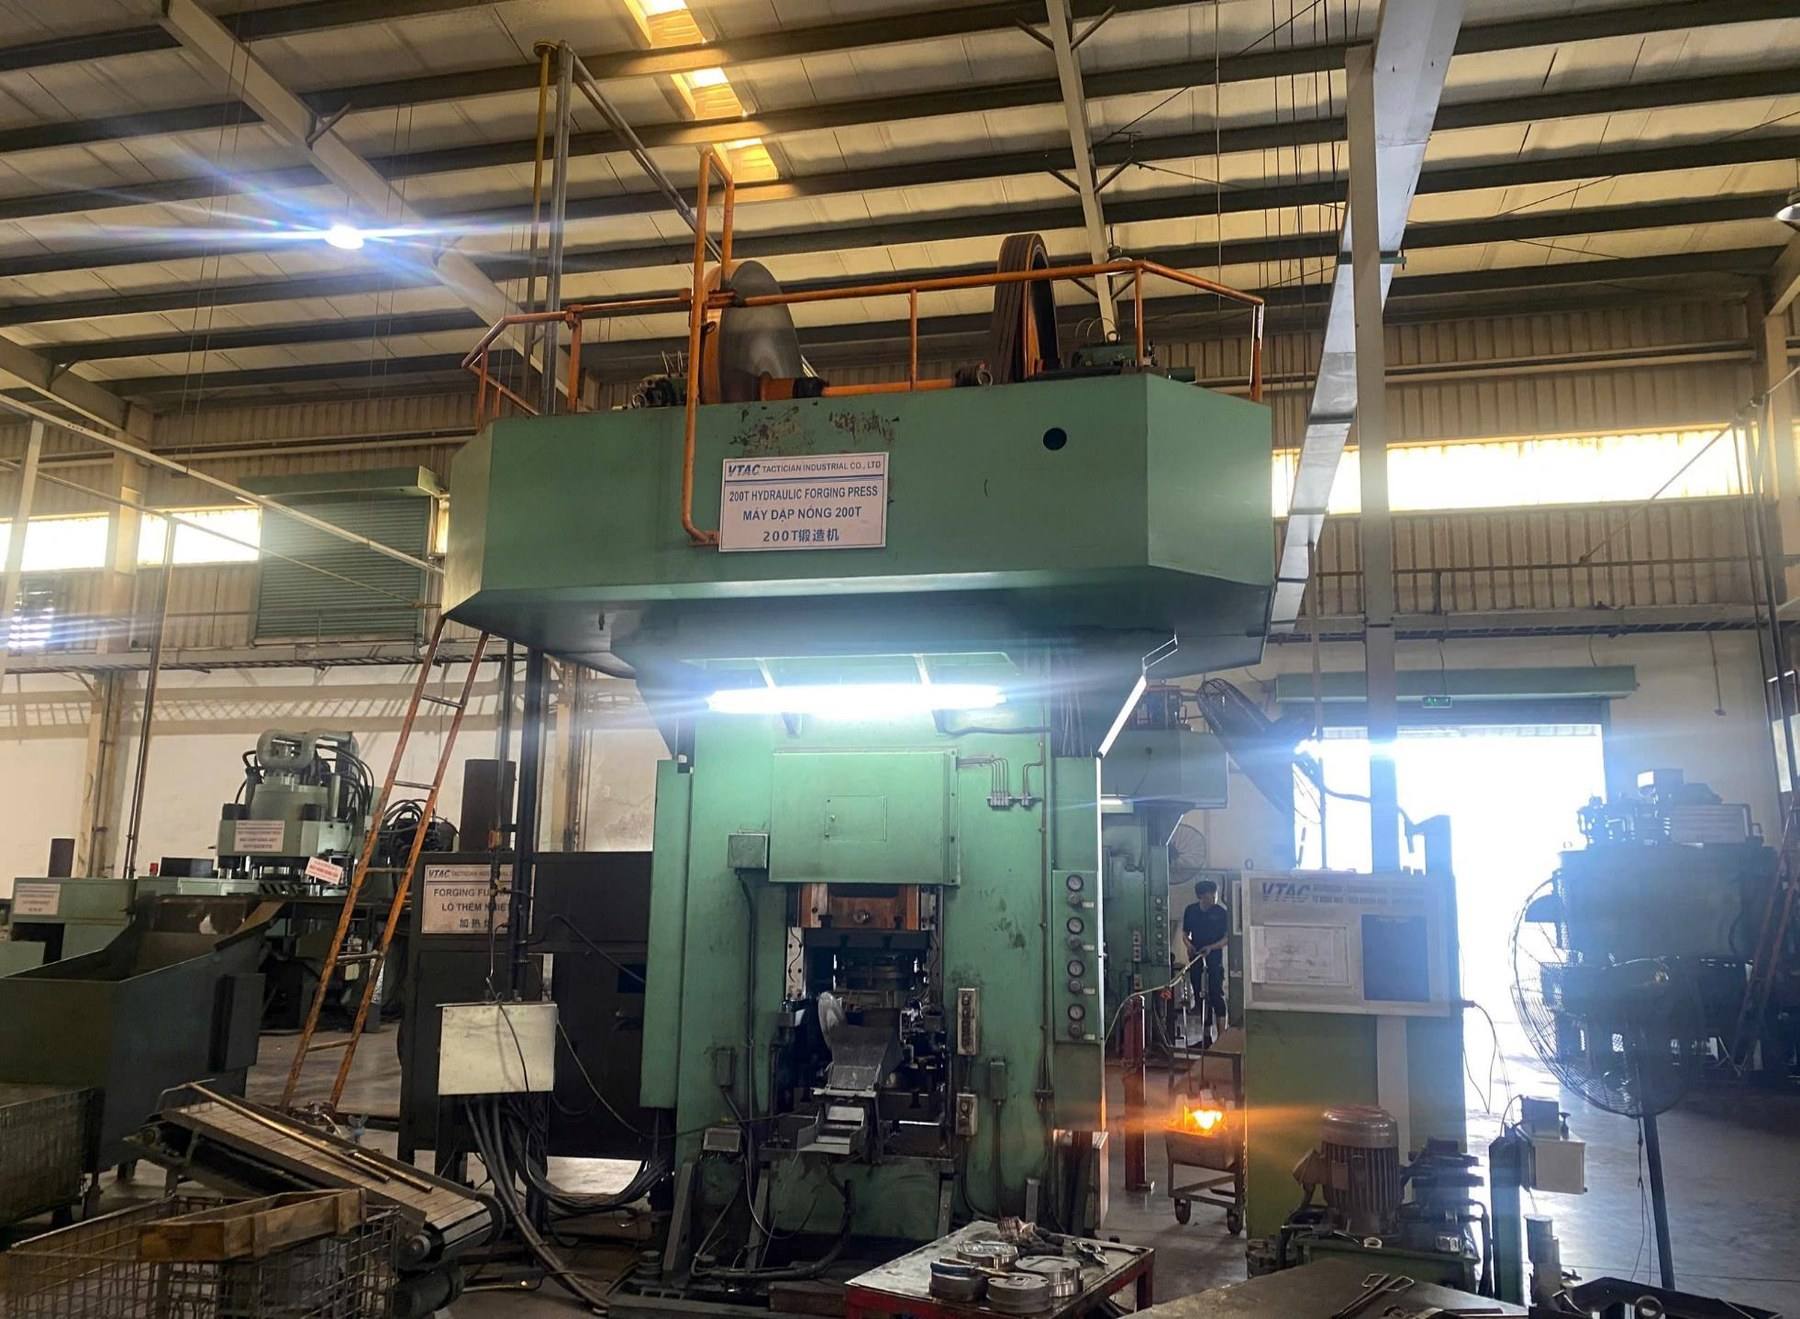
Thai Binh, Vietnam. Production halls, tooling, plating lines, a test laboratory and raw-material warehousing.
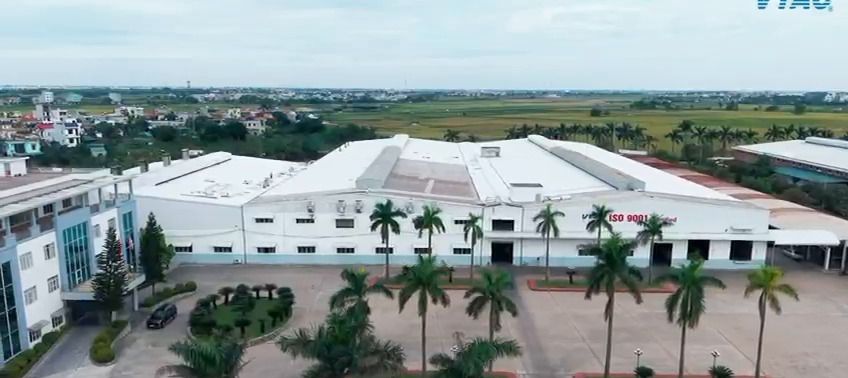
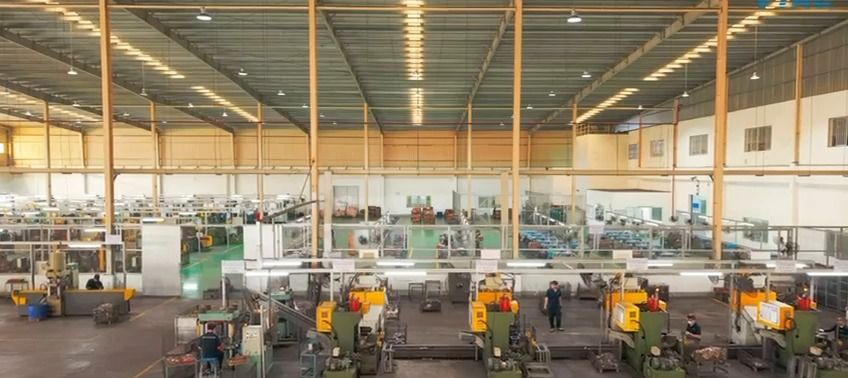
Customers work with one Gold Classic team from the initial concept through production and delivery, supported by our factory in Vietnam. Requirements, drawings and approvals are handled by Gold Classic; the factory turns them into tooling, parts, finishes and packed goods.
The factory operates under the name VTAC. It is where every process described on this page takes place.
01End-to-end process
Nine stages turn a drawing into finished glass fittings and OEM hardware, inside one organisation. Each stage is managed with knowledge of the one before and the one after.
Understanding the application, drawings, material and functional requirements.
Checking structure, assembly and surface effect early, while changes are still inexpensive.
Our in-house tooling facility turns the requirement into moulds, dies and process conditions that can be adjusted and repeated.
Investment casting or hot forging, selected according to geometry, strength, quantity and material.
Dimensions, hole positions and mating faces are machined where the drawing demands control.
Surface flatness, grain and appearance are prepared for the intended finish.
Electroplating and ED coating on our own lines, to the approved colour and surface.
Inspection against drawings, approved samples and the agreed inspection specification.
Assembled and packed according to brand, channel and transport requirements.
02In depth
Casting, Forging & Tooling
Our tooling team works beside casting and hot forging, so a drawing or sample becomes a repeatable component with fewer handovers.
Read the story: Casting, Forging & ToolingPrecision CNC
Hole positions, gasket seats, pin bores and mating faces are machined and checked against the drawing.
Read the story: Precision CNC03Forging capability
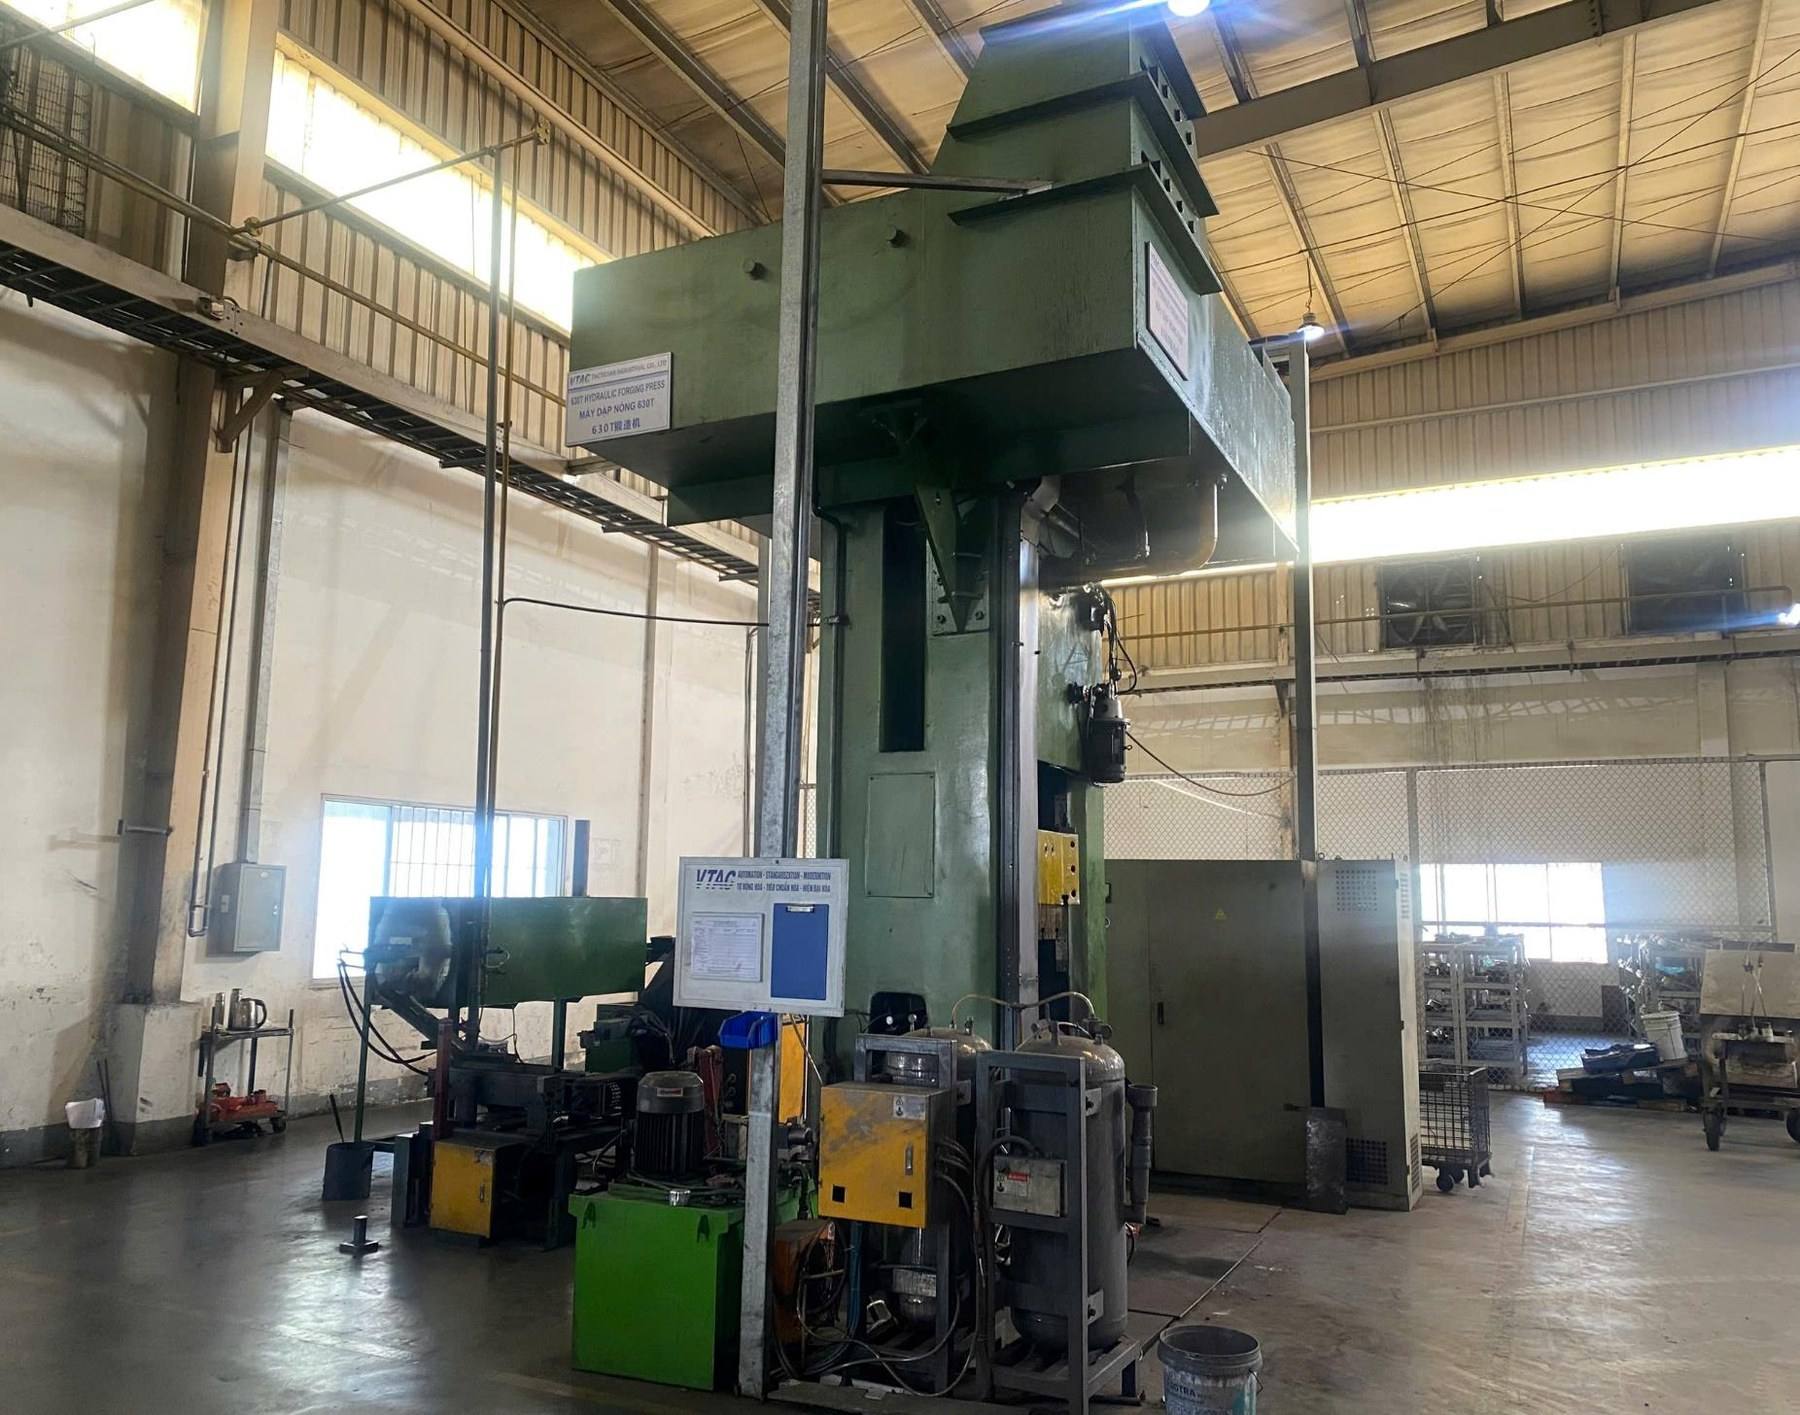
Our forging line supports repeatable production of architectural hardware components, from heated billet and precision tooling through trimming, CNC machining, polishing, plating and final inspection.
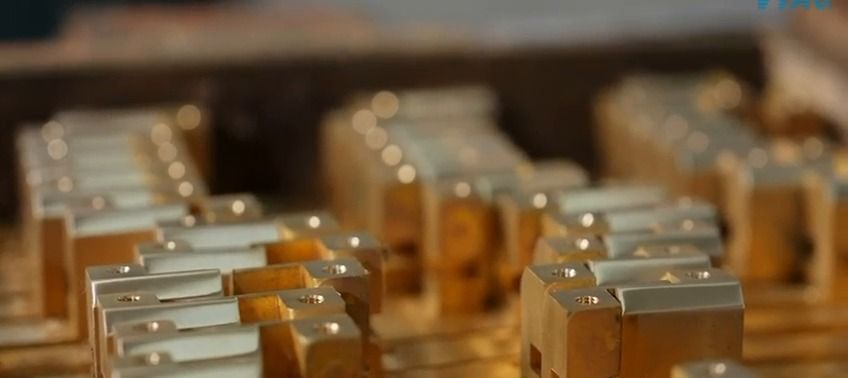
| Press capacity | Quantity |
|---|---|
| 150 t | 1 |
| 200 t | 3 |
| 300 t | 2 |
| 630 t | 1 |
Hot-forging presses. Mechanical transfer arms or FANUC robots assist billet handling on selected presses.
04Finishing
Electroplating and ED coating are operated in-house, directly after polishing. Finishes are approved on physical samples and carried into production against that reference.
05Quality control
Every part is checked against the drawing, the approved sample and the inspection plan. Our factory operates a quality management system to ISO 9001:2015, assessed annually. The current certificate is available on request.
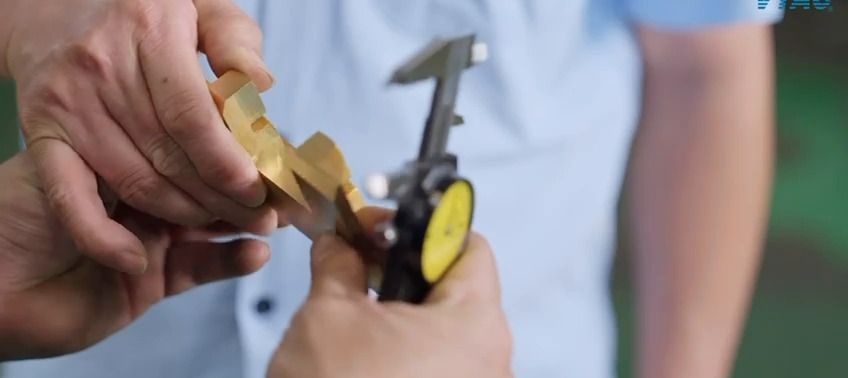
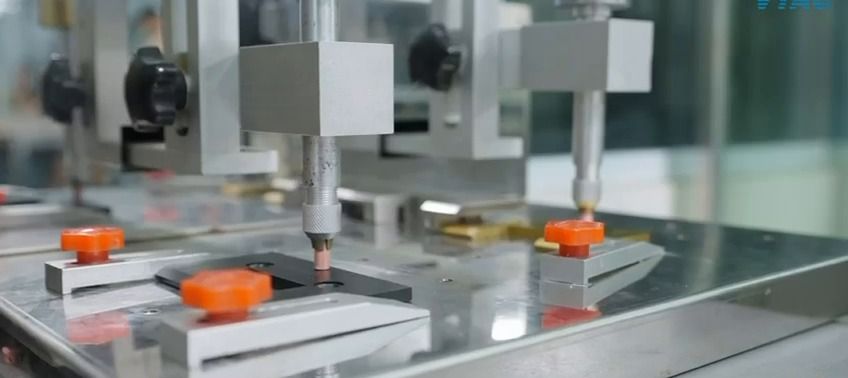
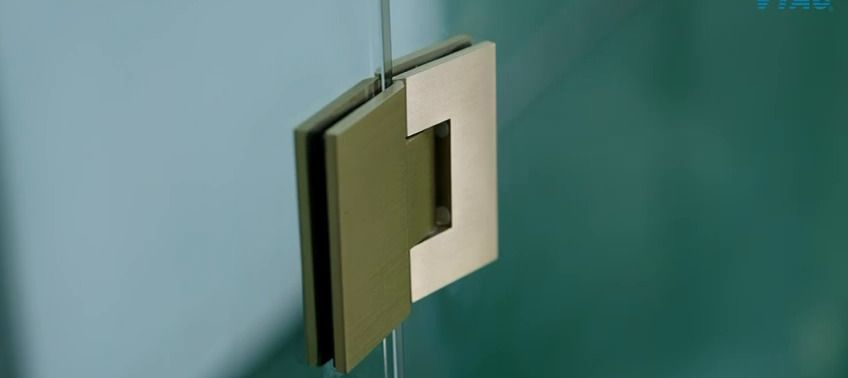
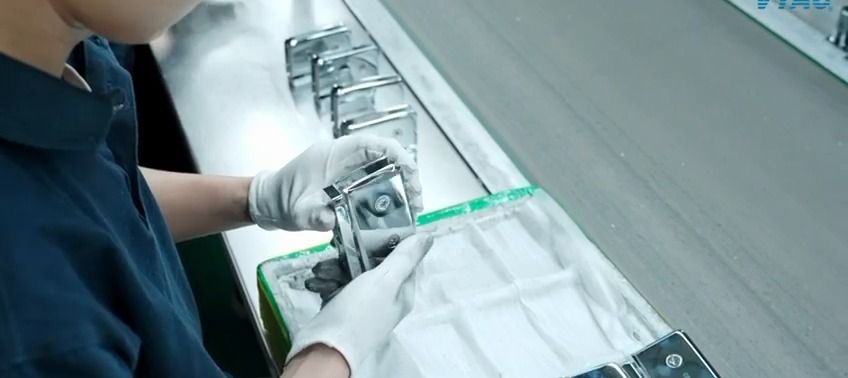
Stills from our 2026 factory film.
06Factory film
A silent excerpt from our 2026 factory film: machining, forging, inspection, polishing, plating and packing. There is no audio track.
Manufacturing
We will review the material, process route and finish with engineering, and reply with a manufacturing path.